Restricted Access Barrier Systems that provide an aseptic, controlled environment for sensitive materials — customized from single workstations to multi-line production.
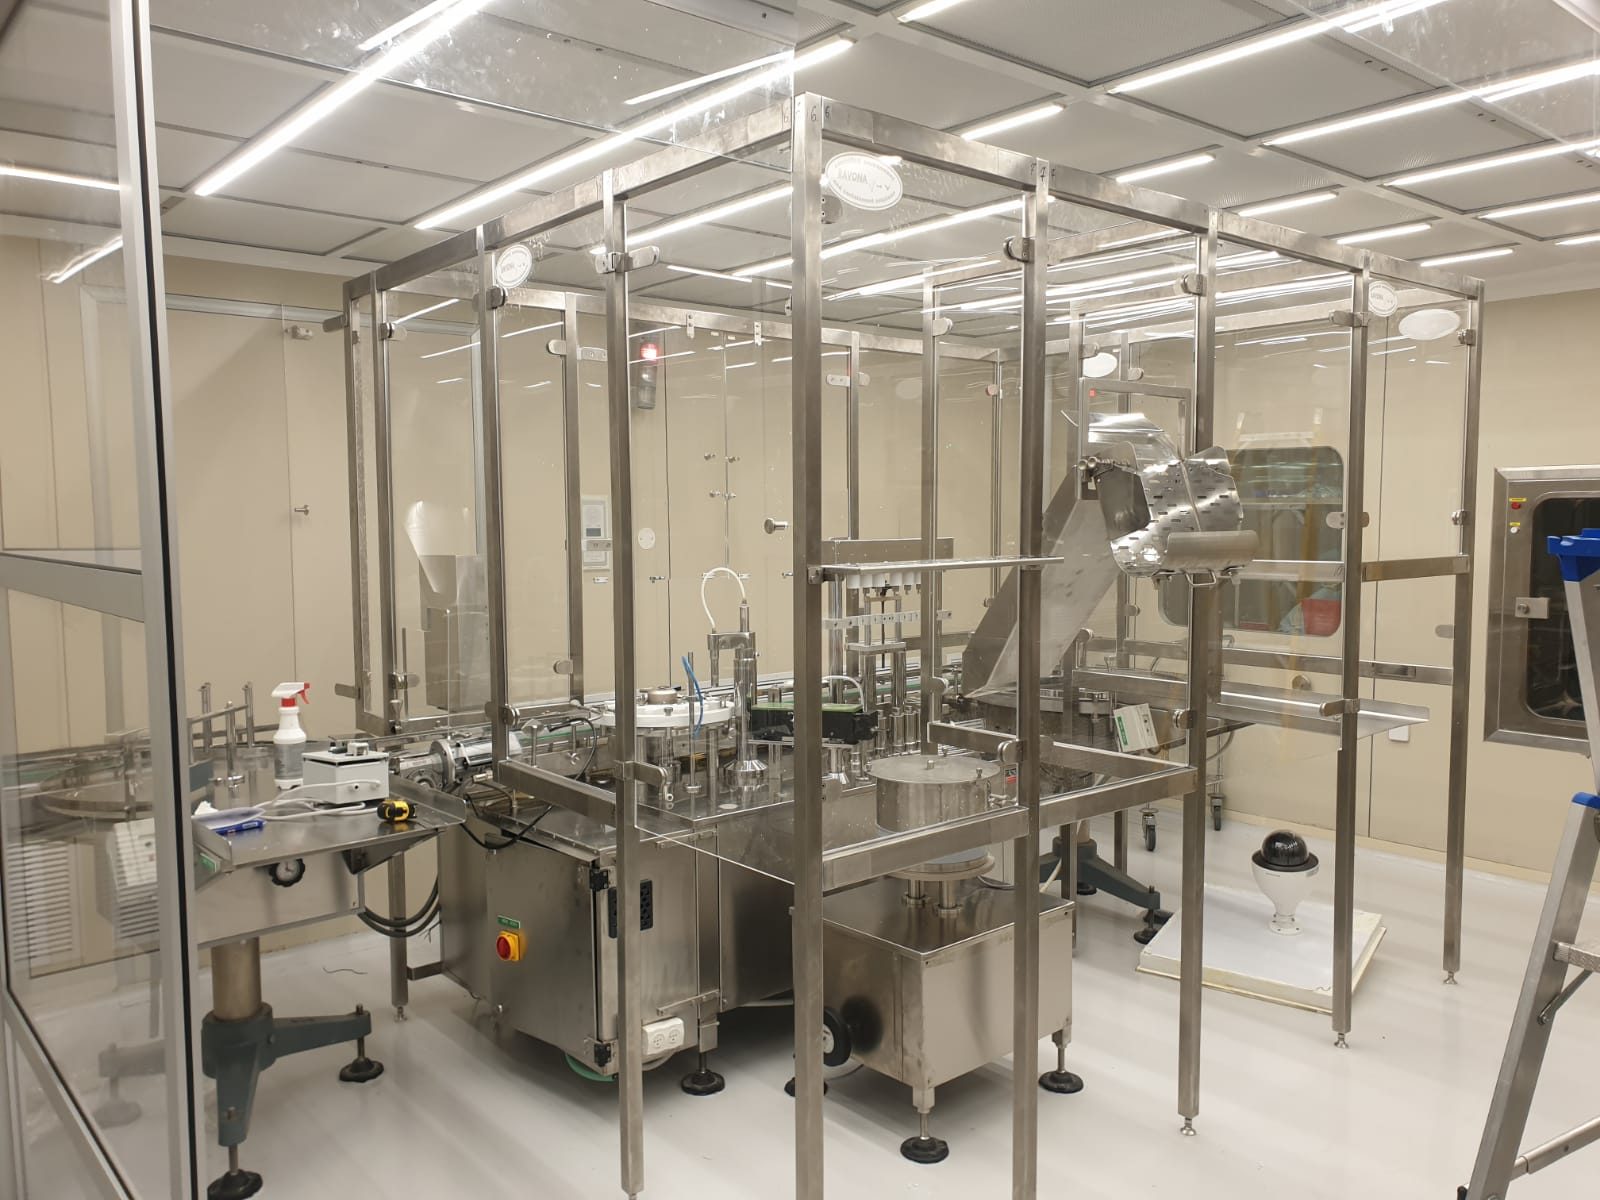
Ravona R.A.B.S create Grade A environments for product handling and protect operators from hazardous materials. Systems are customized to the process, from active systems with enhanced airflow management to passive and modular solutions.
Active airflow management maintains Grade A (ISO 5) with positive pressure and HEPA filtration; suited to fill and finish.
Natural airflow with passive barriers and minimal pressure control; an economical option for smaller-scale or lower-risk processes.
Complete separation between operator and aseptic area with sealed barriers; suited to potent materials, cell and gene therapy and sterility testing.
Barrier between operator and product with easier access through glove ports; suited to small-scale filling, freeze-drying integration and cell culture.
Filter Fan Units cover the critical filling zone evenly, with air speed controlled from the HMI.
Real-time temperature and humidity monitoring to meet aseptic and regulatory requirements.
Systems are designed to comply with FDA, cGMP, ISO and USP requirements.
Ravona is a manufacturer of isolators, R.A.B.S and glove integrity testers. Product information and images are provided by Ravona (aravona.com) and used with their permission. Specifications may vary by configuration; contact us for current details.
Tell us about your process and we will put you in touch with Ravona’s engineers.